7 Tips to Reduce Vibration and Noise Effectively?

Time:2026-10-17 Author:Sienna
0%

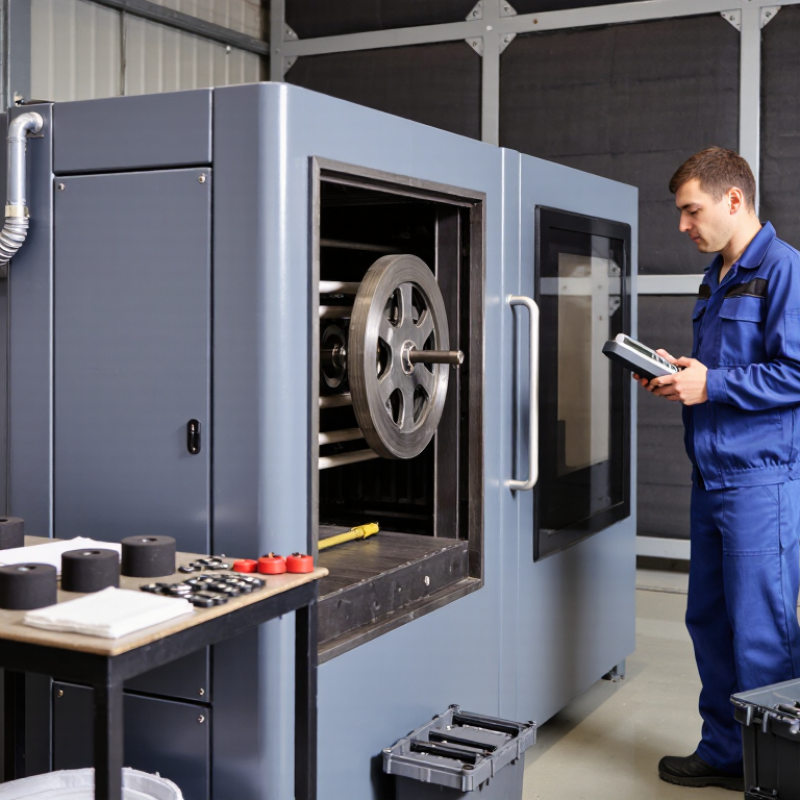
Vibration and noise rarely come from one source. A humming motor, loose fastener, worn bearing, or thin metal panel can create several problems at once. The sound may seem minor beside the machine, yet it can travel through walls, floors, and connected pipes. Effective control begins with finding the transmission path, not simply adding thicker insulation.

This guide explores which solutions reduce vibration and noise effectively in real working environments. It considers practical methods used by maintenance teams, acoustic engineers, and equipment installers. These include resilient mounts, damping materials, enclosure panels, flexible connectors, and regular mechanical inspections. A vibration meter can reveal frequencies that human hearing misses. Even a careful hand check can expose a loose bracket or uneven base.

Small details matter.

However, no single treatment works everywhere. A rubber mount may reduce structure-borne vibration but fail under excessive weight or heat. An acoustic barrier may lower airborne sound while leaving the machine’s physical shaking unchanged. Product ratings also need verification under the actual load, temperature, and operating speed. Some recommendations sound convincing but lack measured evidence. That deserves caution.

The following tips connect proven engineering principles with practical observations from workshops, offices, and industrial spaces. They focus on measurable improvements, safer installation, and long-term reliability. A quieter machine is useful, but a stable machine is better. Noise reduction should never hide a developing fault.
7 Tips to Reduce Vibration and Noise Effectively?

Establish Baselines: Compare Readings with NIOSH’s 85 dBA 8-Hour Limit

Before reducing vibration and noise, establish a reliable baseline. NIOSH identifies 85 dBA as the recommended 8-hour time-weighted average exposure level. This is not a simple pass-or-fail reading. A worker near a cutting station may experience 88 dBA for a short period, then much quieter conditions elsewhere.

Measure at the worker’s ear position, not beside the machine. Use a calibrated sound level meter or personal noise dosimeter, and record the task, duration, and location. The 3 dB exchange rate matters: each 3 dB increase roughly doubles the noise dose. Keep a clear log. Small details matter.

Our first baseline was imperfect. We measured during a quiet production cycle and missed the louder material-loading period. Repeating the survey during normal work exposed the difference. Vibration should be recorded at the hand or seat contact point, using consistent operating conditions. Compare similar shifts, not isolated readings. Then target the source with maintenance, isolation, damping, balanced components, or shorter exposure periods. Hearing protection can reduce risk, but it should not replace engineering controls or regular monitoring. Review readings after every change, because a quieter machine may still transmit harmful vibration. Encourage workers to describe buzzing hands, tingling fingers, or ringing ears; these observations can reveal problems that instruments miss.

Map Sources and Resonance Using FFT and One-Third-Octave Analysis

7 Tips to Reduce Vibration and Noise Effectively?

Map Sources and Resonance Using FFT and One-Third-Octave Analysis

Effective vibration control starts with measurement, not guesswork. Record operating speed, load, location, and the sound heard nearby. Use a calibrated accelerometer and microphone at consistent positions. An FFT spectrum can reveal narrow peaks linked to imbalance, misalignment, looseness, or gear-mesh activity. Mark these frequencies against shaft speed and machine components.

Look for resonance.

A strong response at a small frequency change may indicate structural amplification. Perform a controlled speed sweep when safe, then compare vibration levels across the frame, bearings, floor, and nearby panels. One-third-octave analysis adds a practical view of perceived noise. It groups energy into standardized bands, helping identify whether low-frequency rumble or high-frequency whine dominates. This distinction guides isolation, damping, guarding, or maintenance decisions.

Do not treat every peak as a fault. Background equipment, airflow, and room reflections can distort results. Repeat measurements under matching conditions, and document sensor direction and mounting method. I would also question unusually perfect data; real machinery rarely behaves perfectly. After each adjustment, measure again instead of trusting assumptions. A softer mount may reduce transmitted vibration but increase movement at the source. Reliable decisions come from paired evidence: FFT for precise frequency behavior and one-third-octave data for broader noise exposure and communication.

7 Tips to Reduce Vibration and Noise Effectively

One-third-octave analysis helps identify dominant frequency bands, while FFT measurements can reveal rotating-speed harmonics and resonance peaks. The chart compares representative sound-pressure levels before and after balancing, isolation, damping, and structural corrections.

Values are sound-pressure levels in dB re 20 µPa measured at standardized one-third-octave center frequencies. The largest reductions occur near low-frequency structural resonance and higher-frequency mechanical noise bands.

Install Isolation Mounts Tuned Below One-Third of the Forcing Frequency

7 Tips to Reduce Vibration and Noise Effectively?

Install isolation mounts with a natural frequency below one-third of the forcing frequency. This ratio keeps the system away from resonance and improves isolation during operation. For example, a machine forcing frequency of 30 Hz should use mounts tuned below 10 Hz. At a frequency ratio of three, a properly damped system can reduce transmitted vibration substantially. The result may include less rattling, lower structure-borne noise, and fewer maintenance issues. It is not magic, though. Excessive damping can reduce isolation near the operating frequency.

Measure the machine before selecting mounts. Record running speed, load changes, mounting points, and floor stiffness. A mount that works at 1,800 rpm may perform poorly during startup. The European Environment Agency’s Noise in Europe 2020 report estimated that transport noise causes chronic annoyance for about 22 million people in Europe. That wider finding matters: small mechanical noise sources can add to an already stressful acoustic environment.

Use four mounts only when the load is evenly distributed. Uneven loading can tilt the frame and shift the actual natural frequency. Check static deflection, because softer mounts usually provide lower tuning, but may allow excessive movement. ISO 20816 guidance also emphasizes evaluating vibration severity at defined measurement points. Measure again after installation. Real systems rarely behave exactly like calculations. That is where the design needs honest revision.

Reduce Airborne Noise with Sealed Barriers and STC 50+ Construction

Reducing airborne noise starts with a sealed barrier, not just thicker drywall. Aim for an assembly tested at STC 50 or higher, while remembering that field performance may differ. Sound can travel through tiny gaps around outlets, pipes, ceiling edges, and door frames. Seal these weak points with compatible acoustic sealant. Small openings matter.

Use dense wall layers and separate them from the framing with resilient channels or isolated studs. Keep panel joints staggered between layers, so sound cannot follow one straight path. Fill the cavity with mineral or fiberglass insulation, fitting it gently without compression. Overpacked insulation can reduce its effectiveness.

I have seen carefully built walls fail because one unsealed cable opening was overlooked.

Choose solid-core doors with perimeter seals and automatic door bottoms. Windows should use laminated glass and tight frames where practical. Treat shared ceilings and floors too, because airborne noise may bypass a wall through the building structure. Protect electrical boxes with sealed acoustic enclosures, and avoid placing boxes back-to-back. Inspect every joint under bright light before closing the wall. An STC 50+ target is useful, but it is not a guarantee of silence. Poor workmanship, flanking paths, and rigid connections can still carry voices, television sound, and machinery hum. A final field test can reveal these hidden weaknesses, though testing is sometimes skipped when budgets tighten.

Validate Controls Using ISO 16283-1 and ISO 20816 Measurement Procedures

7 Tips to Reduce Vibration and Noise Effectively?

The European Environment Agency reported that over 113 million Europeans face harmful road-traffic noise above 55 dB Lden. This figure shows why control measures need measured proof, not visual confidence. ISO 16283-1 provides a field method for airborne sound insulation between rooms. It uses defined microphone positions, source-room measurements, receiver-room measurements, and background-noise checks. Record room geometry, equipment status, and weather conditions. Small details can change the result.

Tip 1: Measure before modifying anything. Use repeatable positions and document the operating load. Compare the averaged results with the project’s acoustic target. Do not treat one quiet reading as success. In practice, doors, cable openings, and ventilation paths often defeat thick barriers. ISO 16283-1 helps expose these transmission paths, although poor site control can still weaken confidence.

Tip 2: Separate noise validation from machinery vibration validation. ISO 20816 procedures assess vibration on non-rotating machine parts, using defined measurement locations and operating conditions. Check velocity values, frequency patterns, and changes over time. A stable machine may still create unacceptable room noise. Tip 3: Measure during normal production, startup, and peak load. Tip 4: Repeat readings after isolation mounts, damping layers, or alignment changes. Tip 5: Keep the sensor mounted firmly. Tip 6: Record uncertainty and background conditions. Tip 7: Ask an experienced acoustics professional to review anomalies. Some results will remain imperfect. That is useful; unexplained variation deserves investigation, not removal from the report.

FAQS

Why should vibration and noise be measured before making changes?

Measurement reveals actual sources instead of relying on guesswork. Record speed, load, location, and nearby sounds. Conditions matter.

What can an FFT spectrum reveal?

FFT can show narrow frequency peaks linked to imbalance, misalignment, looseness, or gear activity. Compare peaks with shaft speed.

How can resonance be identified?

Perform a controlled speed sweep when safe. Measure the frame, bearings, floor, and nearby panels. Strong responses after small speed changes may indicate resonance.

What does one-third-octave analysis add?

It groups sound into practical frequency bands. This shows whether low rumble or high-frequency whine dominates. The result guides damping or isolation.

Why is a sealed barrier important for airborne noise control?

Tiny gaps around outlets, pipes, doors, and ceilings can carry sound. Use dense layers and compatible acoustic sealant. Small openings matter.

How can wall and door construction reduce sound transmission?

Use separated framing, staggered panel joints, and gently fitted cavity insulation. Solid-core doors need perimeter seals and automatic door bottoms.

Is an STC 50 or higher assembly guaranteed to be quiet?

No. Field performance can fall because of flanking paths, rigid connections, or poor sealing. A final field test may expose hidden weaknesses.

How should machinery vibration controls be validated?

Measure before and after each adjustment under matching conditions. Check velocity, frequency patterns, operating load, and sensor mounting. Do not trust one reading.

Why should noise and machinery vibration be assessed separately?

A stable machine can still create unacceptable room noise. Airborne sound needs room-to-room testing, while vibration needs measurements on non-rotating machine parts.

Should unusual measurement results be removed from the report?

Not automatically. Background equipment, airflow, reflections, or loose mounting may affect results. Imperfect data can reveal problems worth investigating.

Conclusion

Reducing vibration and noise effectively begins with a clear understanding of existing conditions. Establish baseline readings for sound pressure and equipment vibration, then compare workplace noise exposure with the 85 dBA, 8-hour reference limit. Use FFT and one-third-octave analysis to identify dominant sources, operating frequencies, and resonance points. This information helps determine which solutions reduce vibration and noise effectively rather than relying on trial and error.

For mechanical control, install properly selected isolation mounts with natural frequencies tuned below one-third of the forcing frequency. To limit airborne noise, combine sealed barriers, tight joints, and construction capable of achieving an STC rating of 50 or higher. Finally, validate the improvements through repeatable measurements following ISO 16283-1 for acoustic performance and ISO 20816 for machine vibration. Comparing before-and-after results confirms whether the controls are working and highlights any further adjustments needed for long-term performance.
Sienna

Sienna

Sienna is a skilled marketing professional with a deep expertise in our company’s core products and services. With a passion for innovation and detail, she plays a pivotal role in crafting insightful blog posts that not only highlight the unique features of our offerings but also provide valuable......